Oct 16, 2026Process
What Actually Drives the Price of a CNC Machined Part
Material is rarely the biggest cost in a machined part. The five real price drivers in CNC machining: tolerance, finish, geometry, quantity, documentation.
Introduction
Buyers new to machined parts usually assume the price is mostly material. It rarely is. In most precision components, the metal is a minor share of the invoice — the money is in time: machine time, setup time, measurement time, and the time spent making a rejected part again.
This guide breaks down the five things that actually move the price, roughly in order of impact, so you can tell which of your requirements are worth paying for.
Tolerance — the single biggest lever
Tolerance tightness sets how slowly the machine must run, how many passes are needed, how often the part is measured, and how many parts fall outside the band.
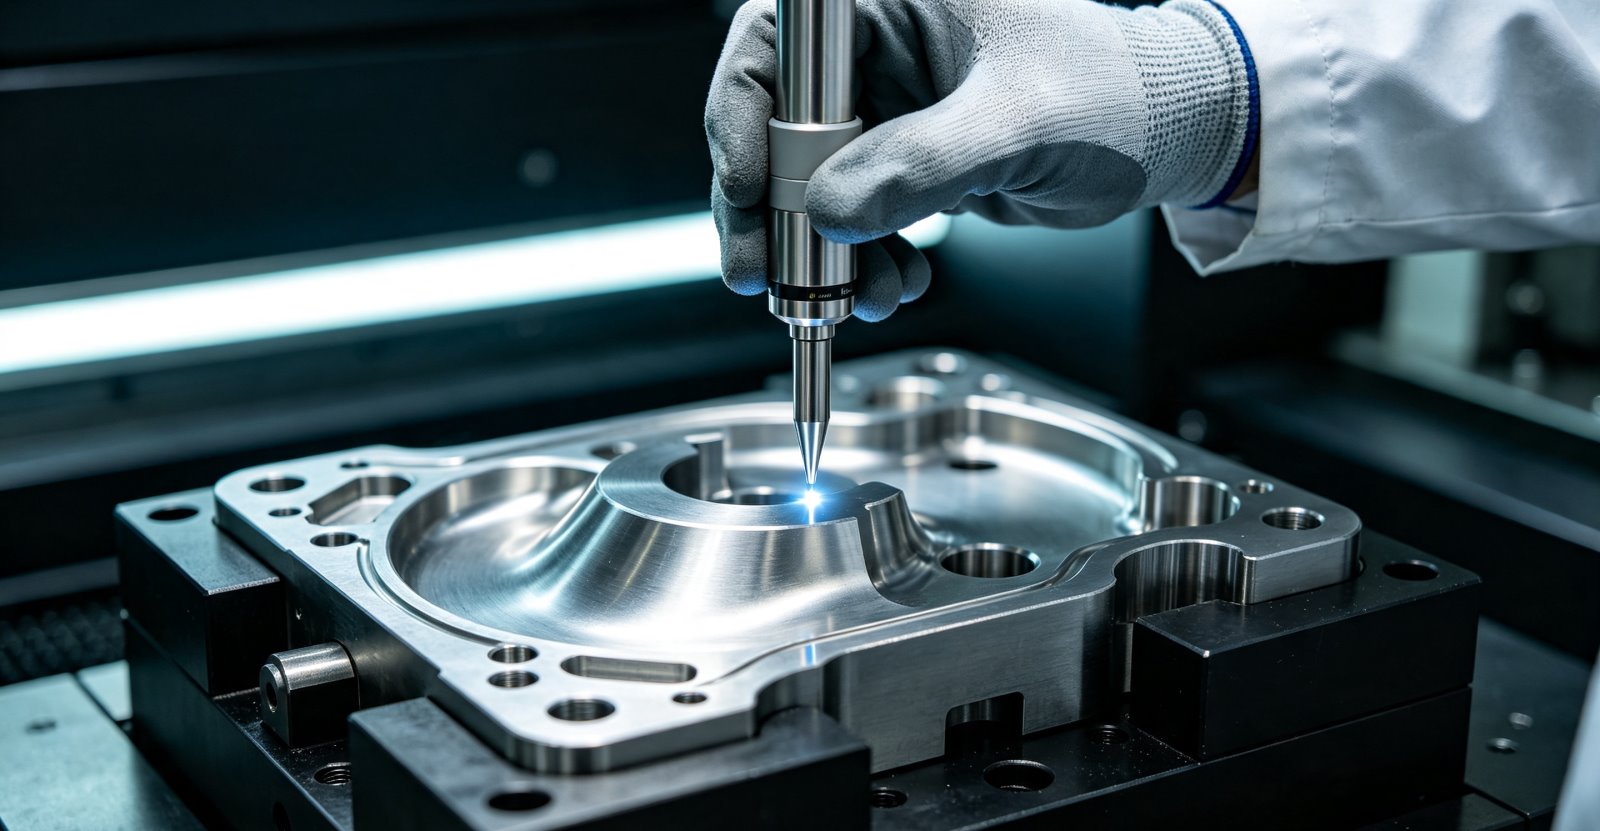
The standard band for most machined features is ±0.01mm to ±0.05mm. High precision — down to ±0.005mm, geometry permitting — means slower finishing passes, controlled temperature, more measurement cycles and a higher rejection risk.
The important part: tightness is usually only needed on a few features — a bore, a sealing face, a locating pin. When a drawing applies a tight general tolerance across every dimension, the price rises and nothing gets better. Put tight bands where function demands them and let the rest live in the standard band.
Surface finish — the invisible multiplier
A surface finish requirement is a machining operation requirement. It adds passes, adds time, and often adds a second process.
As-machined is the baseline. Controlled finishing passes get you to Ra 1.6 or Ra 0.8. Ra 0.4 and below needs fine finishing, dedicated tooling, sometimes polishing after machining. Decorative finishes — anodizing, powder coating, plating, bead blasting — are subcontracted steps with their own cost and lead time.
A common and entirely avoidable cost: specifying a fine finish on faces no one will ever touch. Ask which faces actually need it.
Geometry and setups — where small features get expensive
Price does not scale with part size. It scales with how many times the part must be repositioned.
Deep cavities, thin walls and long slender features require light cuts to avoid chatter and deflection. Features that cannot be reached from one orientation force additional setups — and each setup multiplies both cost and the chance of error. Very small features on small parts need small tooling, slower feeds and more careful workholding.
This is exactly what a DFM review is for: a supplier who reviews your drawing before quoting will often find that one rotated feature eliminates a whole setup.
Quantity — setup cost, spread out
Every job carries a fixed setup and programming cost. At 5 pieces, that fixed cost dominates the per-piece price. At 500 pieces, it nearly disappears.
This creates the single most useful question in machining procurement: “What is the per-piece price at 3x and 5x my quantity?” The answer tells you immediately whether you are paying for setup or for machining — and whether a larger batch is worth the inventory.
It also explains why prototype quotes look high. A prototype is 100% setup and near-zero amortization. That is normal and not a sign of overcharging.
Documentation and inspection — the cost of provability
FAI reports, CMM measurement data, material certificates (CoC), traceability by order number: each of these is real labour. On safety-relevant or regulated parts, this documentation can be a meaningful share of the price.
It is worth paying for where you need it — and worth questioning where you do not. A supplier who can produce verifiable documentation is structurally different from one who cannot; the price difference between them is usually smaller than the cost of discovering the gap after a failed assembly.
What does not drive the price (as much as people think)
Part size alone — a large simple part can be cheaper than a small complex one.
Material choice, within reason — going from 6061 to 7075 aluminium changes cost, but rarely as much as everyone assumes; tightening tolerance across a whole part usually costs more.
Country of origin by itself — what drives offshore pricing is process maturity and documentation discipline, not geography.
Practical summary
Tolerance — the biggest lever. Tighten only where function demands it; keep everything else in the standard band.
Surface finish — specify fine finishes only on functional or visible faces.
Geometry — ask for a DFM review; fewer setups means lower cost and less risk.
Quantity — ask for unit prices at 3x and 5x to see how setup amortizes.
Documentation — keep FAI, CMM and CoC on critical parts; simplify the rest.
Material — consider equivalent grades where performance allows.
Your next step
The fastest way to reduce a machined part's cost is not to find a cheaper shop — it is to have someone who actually machines parts review the drawing and tell you which requirements are expensive and which are unnecessary.
Send your CAD files to Idar Tech in Dongguan, China (ISO 9001:2015, tolerances to ±0.005mm, CMM and FAI reports with 100% inspection on critical parts) for a free DFM review within 24 hours. You will get an itemized quotation with the cost drivers named, not a single unexplained number.